
Pharmaceutical Grade Activated Carbon is not simply charcoal with a cleaner label. It is a carefully manufactured adsorbent designed for controlled pharmaceutical applications, including purification, decolorization, and the removal of unwanted organic compounds. Its value depends on more than high surface area. Pore-size distribution, ash content, moisture, particle size, microbial quality, and extractable impurities all require close attention. A bright powder can still conceal a poor specification.
Professor Harry Marsh, a widely recognized activated-carbon researcher, explained the material’s function in clear technical terms: “Activated carbon is a carbonaceous material that has been processed to develop a porous structure.” That structure resembles an intricate network of microscopic rooms. Contaminant molecules enter these spaces and attach to the carbon surface through adsorption. The process is selective, not magical.
In pharmaceutical production, dependable performance begins with traceable raw materials and controlled activation conditions. Manufacturers should examine certificates of analysis, pharmacopoeial compliance, batch consistency, and supplier validation records. They also need to match the carbon grade with the formulation, process chemistry, and intended contact time. A grade suitable for water treatment may not suit an injectable product or an oral medicine.
The word “pharmaceutical” deserves caution. It does not guarantee universal suitability. Specifications can vary between suppliers, regions, and applications. Even experienced teams may overlook leachables, fine-particle handling, or changes after storage. This article examines what Pharmaceutical Grade Activated Carbon means in practice, how it is tested, and where careful judgment remains necessary. The label helps. Evidence matters more.
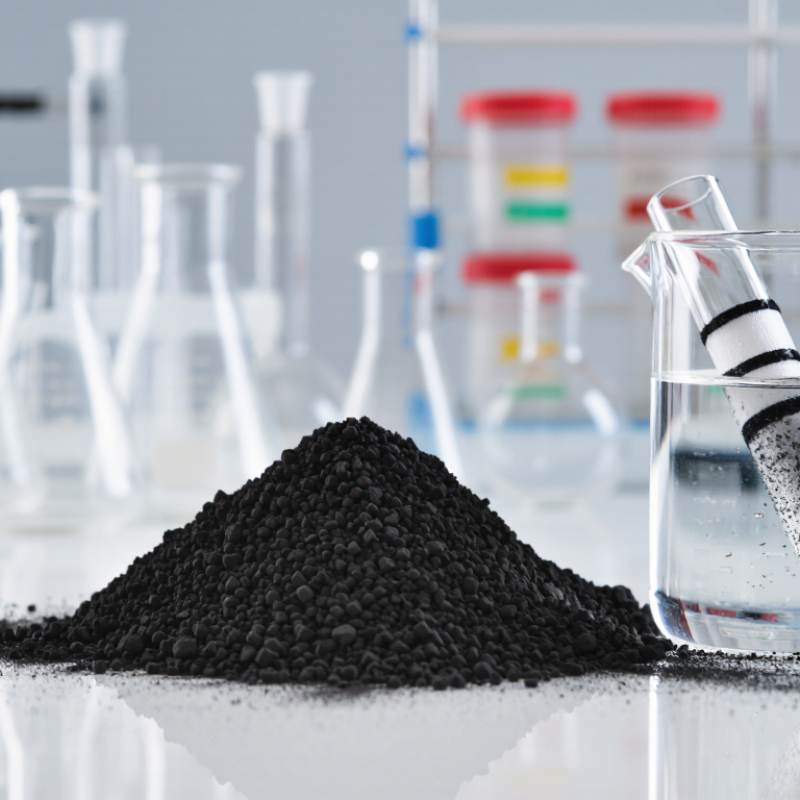
Pharmaceutical grade activated carbon is a highly purified adsorbent used in controlled pharmaceutical processes. It is not simply ordinary charcoal in a cleaner package. Manufacturers select carbon with consistent pore volume, low ash, and limited extractable impurities. Small pores matter. They capture color bodies, organic residues, and unwanted process compounds through adsorption.
The European Pharmacopoeia and United States Pharmacopeia describe quality controls for activated charcoal, including identity, moisture, ash, and impurity-related testing. USP General Chapter <231> has been replaced by elemental impurity controls under USP <232> and <233>, reflecting tighter expectations for metals. The 2023 Grand View Research market report estimated the global activated carbon market at more than US$4 billion, although pharmaceutical applications represent only one specialized segment. That distinction is easy to miss.
In practice, qualification should examine batch records, particle-size distribution, adsorption performance, and microbial controls. A certificate alone is not enough. Testing should match the intended process and dosage form. Carbon may reduce unwanted compounds, but it can also remove active ingredients or excipients. This risk deserves real process data, not assumptions. My own caution is simple: “pharmaceutical grade” is not a universal performance guarantee. It signals compliance with defined specifications, while suitability still depends on validated use, supplier controls, and careful incoming testing.
| Category | Data Dimension | Typical Information | Practical Significance |
|---|---|---|---|
| Definition | Material description | Pharmaceutical grade activated carbon is a highly porous carbon adsorbent manufactured, purified, tested, and packaged for use in pharmaceutical, healthcare, and other regulated processing environments. | Its controlled purity and documented quality make it suitable for applications where contamination control and batch traceability are essential. |
| Raw Materials | Carbonaceous source | Common feedstocks include: Coconut shells Wood Coal | The source and activation method influence pore-size distribution, ash content, hardness, adsorption behavior, and the suitability of the final material for a specific process. |
| Manufacturing | Activation process | Activation is generally performed by steam or carbon dioxide at high temperature, or by chemical activation. The process develops a network of micro-, meso-, and macropores. | A developed pore structure provides a large internal surface area for the physical adsorption of dissolved or gaseous substances. |
| Physical Form | Available forms | Typical forms include: Powder Granules Pellets | Powder is often selected for rapid contact and slurry treatment, while granules and pellets are commonly used in fixed-bed or column systems. |
| Pore Structure | Pore-size classification | Micropores are generally smaller than 2 nm, mesopores are approximately 2–50 nm, and macropores are larger than 50 nm. | Different pore sizes support the adsorption of molecules with different dimensions and affect diffusion into the carbon particle. |
| Adsorption | Primary mechanism | Activated carbon primarily removes substances through surface adsorption, involving physical forces and, depending on the chemistry, stronger surface interactions. | It can reduce color, odor, taste, trace organic compounds, and certain process impurities, but it is not a universal filter for all contaminants. |
| Quality Attribute | Iodine number | The iodine number is commonly reported in mg/g and is used as an indicator of adsorption capacity related mainly to microporosity. A higher value does not automatically mean better performance for every molecule. | The appropriate value depends on the target impurity, solvent or water chemistry, contact time, and process conditions. |
| Quality Attribute | Methylene blue or molasses adsorption | These tests provide information about adsorption in larger pores and can help characterize the carbon’s suitability for relatively larger organic molecules. | They complement iodine testing because adsorption performance is influenced by both pore size and molecular size. |
| Chemical Purity | Ash and extractable substances | Pharmaceutical-use materials are typically controlled for ash, water-soluble substances, acid-soluble substances, pH, and other extractable impurities according to the applicable specification. | Lower and controlled extractables help reduce the risk of introducing inorganic residues or soluble impurities into a pharmaceutical process. |
| Microbiological Quality | Bioburden control | Depending on the intended use, specifications may include total aerobic microbial count, total yeast and mold count, and the absence or limits for specified microorganisms. | Microbiological requirements should be selected according to the process, dosage form, route of administration, and applicable pharmacopoeial or internal standards. |
| Contaminant Control | Elemental impurities | Testing may address metals and other elemental impurities that could originate from raw materials, processing equipment, activation chemicals, or packaging. | Risk-based elemental impurity control supports compliance with applicable pharmaceutical quality requirements. |
| Particle Properties | Particle-size distribution | Particle size is normally specified by sieve analysis or another validated particle-size method. The acceptable range depends on whether the carbon is used as a powder, granule, or fixed-bed medium. | Particle size affects filtration rate, pressure drop, dust generation, adsorption kinetics, and product recovery. |
| Performance | Contact time | Adsorption performance depends on contact time, carbon dosage, temperature, pH, impurity concentration, and the presence of competing substances. | Laboratory testing or process-specific validation is needed to determine the correct dose and operating conditions. |
| Pharmaceutical Uses | Process applications | Common uses include decolorization, odor reduction, removal of trace organic impurities, purification of process water, and treatment of selected pharmaceutical intermediates. | The carbon should be evaluated for compatibility with the product, solvent system, filtration equipment, and downstream purification steps. |
| Medical Use | Emergency oral administration | Activated charcoal may be used in certain poisoning situations under professional medical direction. The decision depends on the substance involved, time since exposure, patient condition, and contraindications. | Industrial or process-grade activated carbon should not be assumed to be suitable for direct human administration unless it meets the relevant medicinal-product requirements. |
| Regulatory Quality | Documentation | A regulated supply may include a certificate of analysis, specification sheet, safety data sheet, manufacturing information, lot identification, test methods, and change-control documentation. | Documentation supports supplier qualification, incoming inspection, deviation management, and batch traceability. |
| Packaging | Protection requirements | Packaging should protect the carbon from moisture, foreign matter, odor contamination, and damage during handling. Sealed, clean, appropriately labeled containers are commonly used. | Proper packaging helps preserve performance and reduces the risk of contamination before use. |
| Handling | Workplace precautions | Powdered activated carbon can generate airborne dust. Local exhaust ventilation, suitable eye protection, protective clothing, and an appropriate respiratory protection program may be required. | Good handling practices reduce inhalation, eye-contact, housekeeping, and cross-contamination risks. |
| Selection | Key purchasing criteria | Important criteria include intended application, raw-material source, activation method, adsorption profile, ash level, extractables, microbiological limits, particle size, moisture, packaging, and batch documentation. | A material should be selected based on demonstrated process performance and the applicable pharmaceutical quality requirements rather than on surface area alone. |


